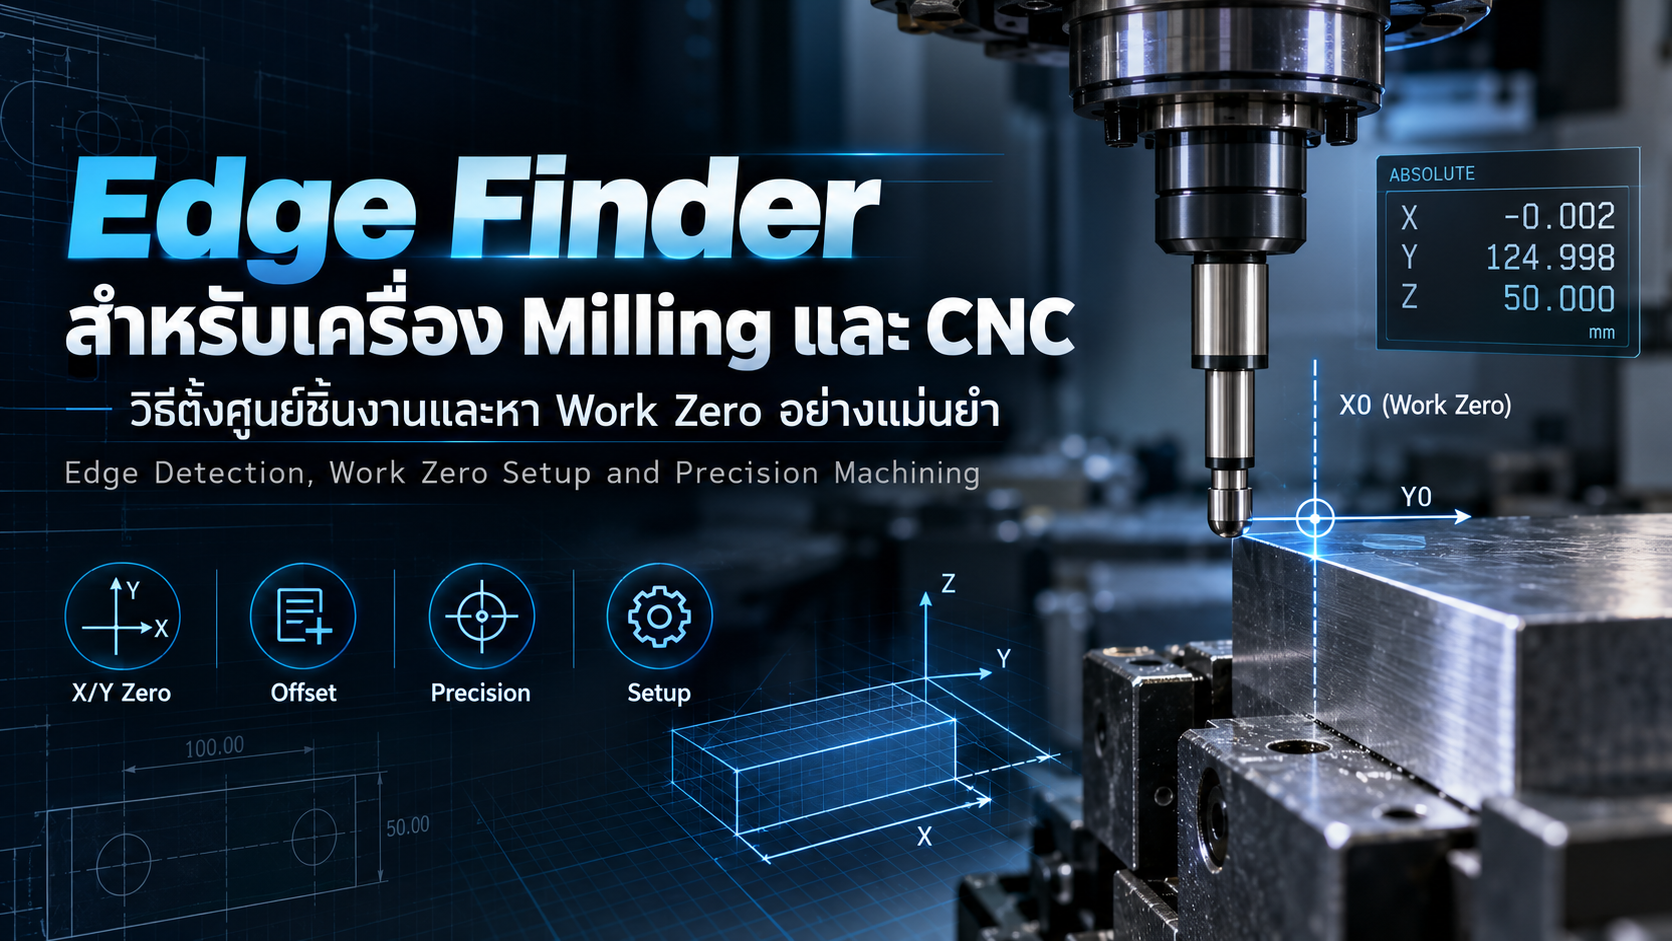
What Is an Edge Finder? How to Set Work Zero on Milling and CNC Machines
A Practical Guide to Edge Detection, Workpiece Zero Setting, Offset Calculation, and Precision Machining
Accurate workpiece positioning is essential for achieving dimensional accuracy in milling and CNC machining operations.
Even a highly accurate CNC machine may produce incorrect features if the workpiece coordinate system is not established correctly.
An Edge Finder is a commonly used setup tool that helps machinists locate workpiece edges, determine reference positions, and establish work zero before machining.
Understanding how an Edge Finder works can improve setup consistency, reduce positioning mistakes, and support precision manufacturing.
1. What Is an Edge Finder?
An Edge Finder is a precision locating tool used on manual milling machines and CNC machining centers.
It is installed in the machine spindle and used to determine the position of a workpiece edge relative to the spindle centerline.
Common applications include:
Locating X-axis and Y-axis workpiece edges
Establishing workpiece zero
Finding the center of a rectangular workpiece
Setting CNC work coordinate offsets
Preparing precision milling operations
The measured edge position can be used to establish a datum according to the engineering drawing or machining program.
2. Types of Edge Finders
Mechanical Edge Finder
A Mechanical Edge Finder uses a spring-loaded contact tip that can move relative to the main body.
When the spindle rotates and the tip approaches a workpiece edge, the contact tip shifts or kicks sideways at the detection point.
This movement provides a reference position for determining the workpiece edge.
Advantages:
Simple mechanical construction
No batteries required
Suitable for manual milling and CNC machines
Generally affordable
Easy to maintain
Limitations:
Requires spindle rotation
Relies on visual detection of tip movement
Requires contact-tip radius compensation
Electronic Edge Finder
An Electronic Edge Finder uses an electrical contact signal to detect a workpiece surface.
When the probe contacts a conductive workpiece, an LED or audible signal indicates contact.
Common electrical-contact models are operated with the spindle stopped.
Advantages:
Clear contact indication
Convenient manual setup
Useful for conductive metal workpieces
Suitable for machining centers and manual mills
Limitations:
Requires battery or electronic power
Electrical-contact models require conductive materials
Insulating coatings can prevent detection
Contact-tip radius compensation is generally required
3D Edge Finder and 3D Sensor
A 3D Sensor can be used to locate reference surfaces along multiple axes, depending on its design.
Some precision 3D sensors allow the operator to position the spindle centerline directly over an edge when the indicator reaches zero.
For example, a properly adjusted HAIMER 3D Sensor can locate an edge without additional probe-ball radius calculations.
Other sensor types may use different referencing procedures, so the manufacturer instructions should always be followed.
3. How a Mechanical Edge Finder Works
A Mechanical Edge Finder operates through controlled spindle rotation and contact between its movable tip and the workpiece surface.
The basic procedure involves four steps.
Step 1 – Install the Edge Finder
Secure the tool in an appropriate collet or tool holder.
Step 2 – Position the Tool
Move the contact tip near the reference edge at a suitable height.
Step 3 – Detect the Edge
Rotate the spindle at the speed specified by the Edge Finder manufacturer.
Carefully approach the workpiece with small axis movements until the contact tip kicks sideways.
Step 4 – Determine the True Edge Position
Record the spindle position and apply the correct contact-tip radius compensation.
The contact-tip diameter, rather than the tool shank diameter, must be used in the calculation.
4. How to Use an Edge Finder on a Manual Milling Machine
For manual milling machines equipped with a Digital Readout (DRO), the procedure typically includes:
Secure the workpiece in a vise or fixture.
Clean the reference surface and remove burrs.
Install the Edge Finder.
Set the spindle speed according to the tool manufacturer's instructions.
Position the tip near the desired edge.
Approach slowly until the mechanical tip kicks.
Record the measured position.
Apply the tip-radius correction.
Establish the required X or Y datum.
Verify the setup before machining.
The workpiece zero location should correspond to the datum defined in the engineering drawing.
5. Setting CNC Work Offsets with an Edge Finder
CNC milling machines use work coordinate systems such as G54 through G59 to define workpiece locations.
An Edge Finder can be used to establish these references manually.
The general procedure is:
Step 1: Secure the workpiece in the machine.
Step 2: Install the appropriate Edge Finder.
Step 3: Select Manual Jog or Handle Jog mode.
Step 4: Locate the X-axis reference edge.
Step 5: Apply the correct contact-tip radius compensation.
Step 6: Record the resulting position in the selected work coordinate system, such as G54.
Step 7: Repeat the procedure for the Y-axis.
Step 8: Verify all work offsets and tool length references before executing the machining program.
The exact offset-setting procedure varies by CNC controller.
Important: Workpiece X/Y positioning and Z-axis tool length compensation are different setup operations and must be verified independently.
6. Edge Finder Offset Calculation
Radius compensation is necessary when using conventional cylindrical-contact Edge Finders.
The basic formula is:
R = D / 2
Where:
R = Contact-tip radius
D = Contact-tip diameter
Example: Ø6 mm Edge Finder
Assume the Edge Finder contact tip has a diameter of 6 mm.
The tip radius is:
R = 6 / 2 = 3 mm
If the spindle center is positioned at X = 97.000 mm when contacting the left side of a workpiece from the negative X direction, the actual edge position is:
X Edge = 97.000 + 3.000 = 100.000 mm
Therefore, the workpiece edge is located at X = 100.000 mm in the coordinate system used for the measurement.
The correction direction must be reversed when approaching the opposite side.
Finding the Workpiece Center
When the two opposite external edges are measured using the same contact-tip diameter:
X Center = (X Left Contact + X Right Contact) / 2
Example:
Left contact position: 97.000 mm
Right contact position: 153.000 mm
X Center = (97 + 153) / 2 = 125.000 mm
The workpiece center is located at X = 125.000 mm.
If the contact-tip radius is 3 mm, the workpiece width is:
Width = 153 - 97 - (2 × 3) = 50 mm
This calculation assumes both edge positions were recorded in the same coordinate system, with the probe contacting the outside of each edge.
7. Edge Finder vs. CNC Touch Probe
Although Edge Finders and Touch Probes are both used for workpiece positioning, their capabilities differ.
Mechanical Edge Finder: A simple solution for manual edge detection and work zero setup.
Electronic Edge Finder: Provides visual or audible contact feedback for conductive workpieces.
3D Sensor: Supports multi-axis surface location and measurement, depending on its design.
CNC Touch Probe: Can work with CNC probing cycles to automate workpiece positioning, dimensional checks, and work offset updates.
For repeated production runs, integrated CNC probing systems may reduce setup time and operator-dependent errors.
8. Common Edge Finder Setup Errors
Several factors can reduce measurement consistency.
Worn Contact Tip
A damaged or worn tip may change the effective contact diameter.
Tool Holder Runout
Excessive runout can affect measurement repeatability.
Dirty Workpiece Surface
Burrs, chips, and contamination may produce incorrect reference positions.
Excessive Approach Speed
Moving too quickly near the workpiece edge can result in inaccurate detection or tool damage.
Incorrect Radius Compensation
Applying the contact-tip radius in the wrong direction can shift the programmed machining origin.
Incorrect Work Offset Selection
Entering a reference position into the wrong work coordinate system may cause significant positioning errors.
Machinists should verify the measuring tool, work offset selection, setup procedure, and required machining tolerances before starting production.
9. Edge Finder Safety Guidelines
Safe setup practices are essential during machining operations.
Follow the manufacturer's spindle speed limits.
Use small jog increments near contact.
Never touch a rotating Edge Finder.
Keep hands away from rotating components and moving axes.
Confirm workholding stability.
Check for collisions with fixtures and machine components.
Verify work coordinate and tool length offsets.
Follow machine guarding and workshop safety procedures.
A careful setup process can help prevent equipment damage and reduce operational risks.
10. Conclusion
An Edge Finder is an important workpiece setup tool for manual milling and CNC machining.
It allows machinists to establish accurate reference positions before machining operations begin.
Understanding edge detection, contact-tip radius compensation, work coordinate systems, and safe setup practices helps improve machining consistency and reduce avoidable errors.
Whether using a Mechanical Edge Finder, Electronic Edge Finder, or advanced 3D Sensor, accurate datum setting remains a fundamental part of precision manufacturing.
Accurate workpiece positioning is the foundation of reliable machining.
AC DESIGN AND DEVELOPMENT – Engineering & Industrial Solutions
AC DESIGN AND DEVELOPMENT CO., LTD. provides custom engineering and manufacturing solutions for industrial applications.
Our services include:
Automation Machine Design and Manufacturing
Custom Jig & Fixture
Machine Parts Manufacturing
Conveyor Systems
Industrial Steel Structures
Custom Engineering Solutions
We focus on practical engineering solutions that support manufacturing efficiency, production quality, and process reliability.
Engineering and Manufacturing Solutions Across Thailand
Website: https://acdesignanddevelopment.com/
Tel: +66 82-210-0792
Technical Disclaimer: This article is intended for educational purposes. Always refer to the machine manufacturer's manual, Edge Finder specifications, and applicable workshop safety procedures.